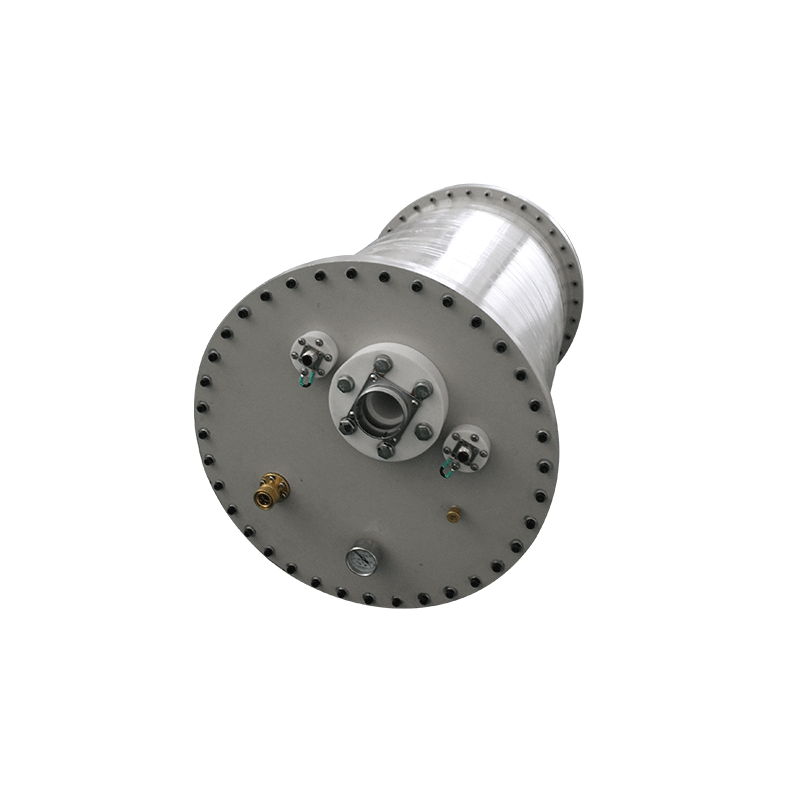
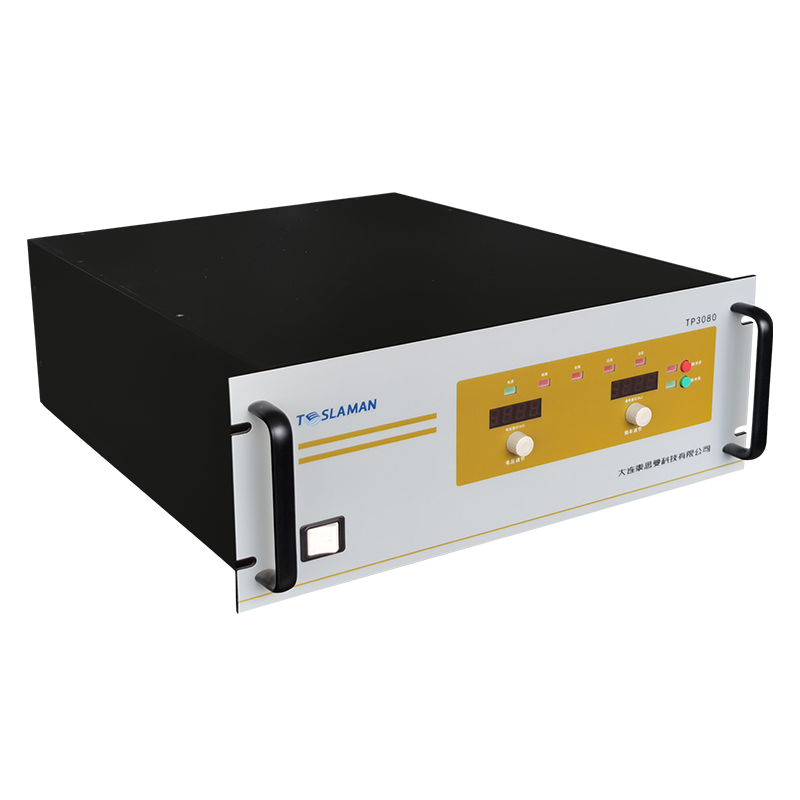
Electron Beam System High-Voltage Power Supply Energy in Material Surface Hardening and Microelectronics Modification
Electron beam systems harden material surfaces and modify microelectronic layers through controlled energy deposition. The beam energy comes from the accelerating voltage, and the supply that establishes this voltage determines the depth of penetration and the dose delivered to the target. Surface hardening of tool steel and modification of thin films both rely on the same disciplined control of the accelerating potential.
Penetration depth scales with accelerating voltage. A higher voltage pushes the beam deeper, which suits case hardening of thick sections, while a lower voltage keeps the energy near the surface for thin-layer modification. The supply must hold the selected voltage without sagging as the beam current rises, because a drooping voltage changes the depth profile mid-process and ruins the uniformity.
Beam current and voltage are regulated together in the power loop. The product of the two defines the deposited power, and the loop maintains this product against variations in cathode emission and target temperature. Constant-power regulation simplifies process recipes, since the operator enters one power value and the supply settles the voltage-current pair for the prevailing gun condition.
Transient behavior matters during process start and stop. The beam is often blanked between passes, and each blanking cycle loads and unloads the supply. The control loop must recover from the load step without overshoot that could momentarily double the deposited dose; measurements on a production unit show settling within a few milliseconds and overshoot below one percent.
Ripple on the accelerating voltage modulates the beam energy slightly. For surface hardening the effect is minor, but for microelectronic modification where layer thickness depends on dose, ripple produces thickness variation. The output filter is therefore sized to keep ripple below the level where dose variation exceeds the process tolerance, and filter aging is monitored through the ripple readback.
Arcing inside the gun or the beamline is an unavoidable event. The supply must detect the arc current rise, extinguish the discharge by collapsing the output, and then reapply the voltage after a defined recovery interval. The recovery sequence is programmable because different applications tolerate different dead times; short recovery suits high-throughput hardening, while delicate substrates need a gentler reapplication.
Long-term stability of the accelerating voltage holds the process window over time. The high-voltage reference and the feedback divider are the stability-critical parts, and both are selected for low drift and matched temperature behavior. Verification records track the output against a calibrated standard, and corrective adjustment is scheduled before drift consumes the process margin.
Safety systems complete the installation. The beamline is interlocked so that the accelerating voltage can only be applied when vacuum and cooling conditions are satisfied. The interlock chain is hardwired and independent of the control software, and the discharge resistor bleeds stored energy within a defined time so maintenance can begin safely after shutdown.
Calibration management covers the measurement channels used by the supply and the instruments used to verify the supply. Each channel has a calibration interval and a tolerance, and the calibration records are traceable to the laboratory standards. The calibration status is checked before a critical measurement campaign starts.
Documentation control ensures that the drawings, the manuals, and the configuration records reflect the installed equipment. Any modification is documented with the change reason and the verification result. The document set is reviewed at planned intervals, and the obsolete versions are archived rather than discarded.
Spare parts management matches the stock level to the failure statistics of the equipment family. The fast-moving parts are kept on site, and the slow-moving parts are sourced on demand. The stock review is performed quarterly, and the review data include the part cost and the delivery lead time.
Safety procedures around the high-voltage equipment are written, reviewed, and rehearsed. The procedures cover the access control, the discharge sequence, and the use of personal protective equipment. The rehearsal results are recorded, and the procedure is revised when the rehearsal reveals a gap.
Environmental control in the equipment room stabilizes the operating conditions of the supply. The temperature and the humidity are monitored continuously, and the alarm thresholds are set to protect the insulation and the electronics. The environmental records are kept alongside the equipment log for the correlation analysis.
Data analysis turns the logged operating data into maintenance decisions. The voltage, current, temperature, and alarm trends are reviewed at planned intervals, and the deviations from the baseline trigger an investigation. The analysis report is shared with the engineering team and the maintenance crew.
Reliability assessment uses the field data collected from the equipment population. The failure rate, the repair time, and the availability are computed over a rolling period, and the results are compared with the design targets. The assessment output feeds the capital replacement plan and the spares strategy.
Energy efficiency of the supply affects the operating cost and the cooling load. The efficiency is measured at the representative operating points, and the improvement opportunities are evaluated against the implementation cost. The efficiency records are maintained for the lifetime comparison.
Training programs for the operating and maintenance staff are scheduled at defined intervals. The training covers the safe operation, the routine checks, and the fault diagnosis flow. The training effectiveness is verified with a written test and a practical exercise, and the results are filed with the personnel records.
Process qualification is performed whenever the equipment or the process recipe changes. The qualification plan defines the test articles, the acceptance criteria, and the data to be recorded. The qualification report is approved before the new condition enters production.
Failure analysis follows a defined path from the symptom to the root cause. The analysis uses the logged data, the physical evidence, and the repair records. The analysis conclusion is documented with the corrective action, and the corrective action is verified after implementation.
Quality records link the equipment performance to the product quality. The operating parameters and the product measurements are filed together, so that a product deviation can be traced to the equipment condition. The record retention period follows the regulatory and contractual requirements.
Vendor coordination covers the technical support, the spare supply, and the repair service. The service level agreement defines the response time and the repair turnaround. The vendor performance is reviewed periodically, and the review outcome influences the future procurement decisions.