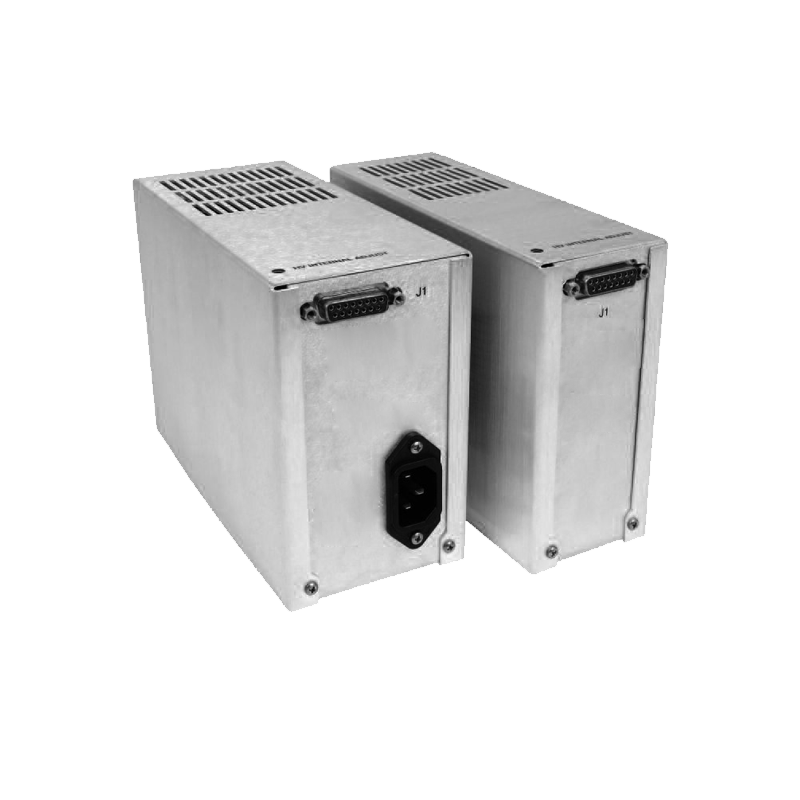
Long-Term Reliability Testing of Ion Implantation High-Voltage Power Supply for High-Voltage Stability in Chip Manufacturing
Long-term reliability testing of an ion implantation supply focuses on high-voltage stability under continuous duty. The implant process tolerates no voltage excursion, and the test program covers aging, cycling and environmental stress over a representative period.
The aging run applies rated voltage and current continuously. Output voltage, output current, ripple and internal temperatures are logged, the daily drift is extracted, and any excursion beyond the specification stops the test for root-cause analysis.
Load cycling simulates the batch process. The load is stepped between standby and implant current thousands of times, the voltage recovery is measured at every step, and the recovery time distribution shows whether the loop holds the stability margin.
Temperature cycling stresses the insulation and the divider. The unit is cycled across the operating temperature range, the divider ratio is measured before and after each cycle, and the ratio shift stays below the calibration tolerance over the whole program.
High-voltage components carry the main aging risk. The multiplier capacitors and the rectifier diodes are monitored through the test, the temperature rise is recorded, and component-level data links the electrical aging to the thermal condition.
Partial discharge is measured at intervals during the test. The discharge level is compared with the initial baseline, a rising trend is investigated immediately, and the insulation margin is confirmed at the end of the program.
Protection functions are exercised repeatedly. Overcurrent and overvoltage faults are injected, the action time is recorded each time, and the protection chain demonstrates repeatable behavior without false trips during normal operation.
The vacuum interface of the implant column is part of the test. The cable and the feedthrough are included, the corona onset is checked at the interface, and the test verifies that the connection design sustains the rated voltage in service.
Grid quality affects the observed stability. The supply is tested across the input voltage range, brownout recovery is verified, and the test data defines the minimum grid condition under which the guaranteed stability holds.
Statistical analysis closes the test program. Failure rate, dominant fault mode and drift distribution are extracted, the dominant mode is corrected, and the corrected unit repeats the affected portion of the test before the final acceptance.
Field data from the first production period is compared with the test results. Early-life failures are matched against the findings, the corrective actions are verified, and the comparison confirms that the reliability target is met in service.
The test archive keeps raw records and conclusions. Traceability from the test plan to the acceptance decision is complete, and the archive supports reliability audits and future design improvements.
Current sharing among paralleled devices decides module reliability. Matching and balancing resistors are combined, sharing deviation is monitored online, and derated operation with a maintenance order follows when the limit is exceeded.
The distributed parameters of the output cable affect dynamic performance. Cable capacitance joins the load characteristic, long cables need a buffer network at the load end, and step-response testing corrects the design.
Voltage transitions during process change require ramp control. Step transitions shock the load, the ramp time is set from the process tolerance, and transition records are retained for traceability.
Insulating oil or gas monitoring reveals deterioration early. Dielectric strength, moisture and gas content are tested on a schedule, shutdown follows when a limit is crossed, and insulation breakdown is prevented.
Switch driver reliability decides overall stability. Drive voltage and current margins are verified, dead time is optimized, and driver faults are linked to the protection chain.
Time-domain and frequency-domain ripple measurements complement each other. The waveform shows the peak-to-peak value, the spectrum locates the components, and the two together guide the filtering correction.
Core saturation causes inductor failure and ripple rejection degrades along with the core condition. Core gap and operating flux density are verified at the design stage, and inductor current monitoring gives early warning of the saturation trend.
Voltage distribution across the capacitors of a multiplier stage needs balancing measures. Balancing resistors equalize the static distribution, capacitance matching controls the dynamic distribution, and voltage measurement confirms the result.
After relocation the insulation and grounding must be re-verified. Transport vibration can loosen connections, and the unit returns to service only after a new withstand test and a grounding check.
Separation of the control power from the power stage improves reliability. The control circuit has an independent feed, a power-stage fault does not disturb the control logic, and the post-fault state remains clearly defined.
Inrush at start-up is limited by a precharge circuit. A precharge resistor works with a bypass contactor, the bypass closes after precharge completion is confirmed, and contactor switching under load is avoided.
Data record resolution and sampling rate match the analysis needs. Slow trends and fast events are stored separately, and the event record keeps the waveform before the fault.
High-altitude application derates both insulation and cooling. Thinner air lowers the breakdown voltage and the cooling capability, design parameters are corrected by altitude, and test conditions simulate the site.
A power factor correction stage improves the grid-side behavior. Input current harmonics drop, reactive losses fall, the grid capacity requirement decreases, and harmonic testing verifies the result.
Product consistency is guarded by factory testing. Voltage accuracy, ripple, protection action and temperature rise are verified unit by unit, test data is archived, and batch variation is analyzed statistically.
Spare parts management follows the failure statistics. High-failure parts carry higher stock, long-lead parts are reserved in advance, and downtime shortens.
The remote maintenance channel needs security design. Permission levels, operation audit and data encryption are enforced, remote operations confirm the site condition first, and misuse risk stays bounded.
Residual charge discharge time at the output enters the safety procedure. Maintenance starts after the discharge completes, and the discharge indicator works with the mechanical interlock.
Online and offline insulation measurements complement each other. Online monitoring reflects the dynamic state, offline measurement gives absolute values, and the combination evaluates insulation health.
High-frequency noise is suppressed through the dual channels of shielding and filtering. Shielding blocks the radiation path, filtering attenuates the conducted path, and the two together meet the whole-unit specification.
Process parameters and supply parameters are archived together. Recipe numbers, voltage and current settings and batch results are linked, parameter changes leave traces, and quality traceability stays complete.