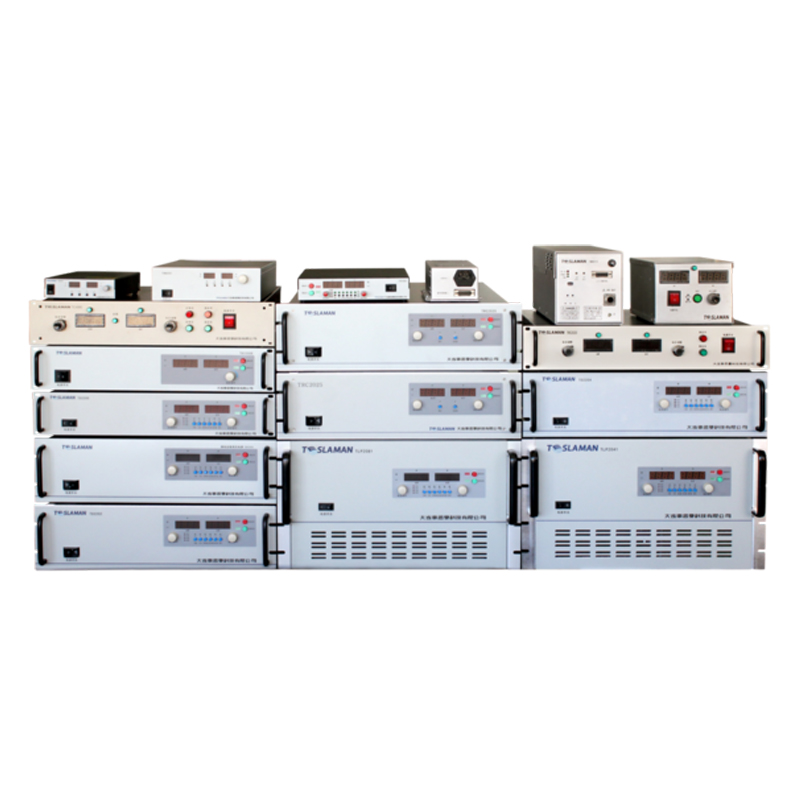

Microchannel Plate Detector High-Voltage Power Supply in Industrial Radiation Detection and Radiation-Tolerant Environment
The microchannel plate detector supply in industrial radiation detection and radiation-tolerant environment keeps the detector gain repeatable for the counting application. The detection depends on the stable gain, so the supply holds the plate voltage and the calibration is verified by the standard source.
The plate voltage stability sets the gain. The voltage is held by the loop, the gain is repeatable, and the count rate is consistent.
The low noise floor keeps the single-event detection sensitive. The filter and the shield reduce the interference, the dark count is bounded, and the signal threshold is verified.
The radiation-tolerant design covers the electronics. The component selection follows the dose requirement, the failure mode is analyzed, and the operation window is defined.
The supply protection covers the detector faults. The overvoltage and the overcurrent are handled, the plate is protected, and the recovery follows the defined sequence.
The calibration uses the reference source. The gain is measured, the deviation is corrected, and the traceability is archived.
The process verification uses the count measurement. The count rate is compared with the standard, and the plate voltage is adjusted from the result.
Field maintenance focuses on the high-voltage chain and the detector state. The gain is verified periodically, and the anomaly is located from the record.
The long-running equipment gets the periodic inspection. The temperature, the noise, the vibration and the drift are recorded, the trend is built, and the anomaly is found early.
The test fixture life is managed. The worn fixture shifts the test result, the fixture is replaced by the count or the period, and the calibration verifies the state.
The environment condition during the test is recorded. The temperature and the humidity affect the insulation and the accuracy result, and the condition is written into the report.
The report conclusion corresponds to the data. The conclusion is derived from the data, the conclusion is not made from the incomplete data, and the data integrity is checked first.
The operator training follows the standard work instruction. The step, the criterion and the abnormal handling are consistent with the actual action.
The traceability system manages by the batch. The test data of each unit is linked to the serial number, and the problem is traced back to the specific batch and stage.
The field measurement of the power factor requires the calibrated wattmeter. The wattmeter is verified against the standard source, and the measured value is compared with the calculated value.
The load regulation measurement is done at the defined load step. The output change between the no-load and the rated load is recorded, and the regulation value is judged against the specification.
The test bench grounding and the shielding are done first. The interference enters through the ground loop and the space path, the bus bar cross section decides the reading stability, and the shield continuity decides the ripple measurement quality.
The calibration interval follows the usage frequency. The instrument used daily is calibrated every three months, the instrument used occasionally every six months, and the certificate is archived for the field trace.
The electronic load differs from the real load. The resistive load changes with the temperature, the electronic load carries the equivalent capacitance, and the conclusion is verified under both conditions.
The test cycle and the test depth conflict on the line. The tight cycle leaves the item untested, the long test cuts the throughput, and the failure risk decides the allocation between the line test and the sample test.
The aging condition follows the field data. The temperature, the humidity and the grid fluctuation are set from the record, the accelerated condition shows the real margin, and the distorted condition gives the useless life data.
The data recording habit decides the fault location speed. The voltage, the current, the temperature and the time stamp are recorded together, and the complete data chain is more useful than the later guess.
The spare part stock follows the module failure rate. The high-failure module is stocked more, the low-failure module less, and the balance is found between the capital and the downtime loss.
The field check starts from the supply source. The input waveform, the grounding state and the grid fluctuation are checked first, the source is clean before the equipment is examined, and the reversed order leads to the wrong judgment.
The repair record contains the phenomenon and the action. The same phenomenon may match different root causes, and the complete record builds the judgment experience.
The meter range is chosen with the margin in mind. The range close to the measured value saturates the reading, the range with too much margin loses the resolution, and the small deviation is missed.
The safety distance follows the voltage level. The higher voltage needs the larger distance, the fence and the warning sign are kept, and the emergency stop is placed within reach.
The contact resistance of the test lead and the fixture affects the result. The poor contact adds the drop into the reading, the fixture is cleaned and replaced periodically, and the contact state is checked by the drop method.
The temperature rise data of the aging test is judged at the thermal steady state. The temperature rises to the stable value before the record, the short energizing time gives the low rise and the optimistic conclusion.
The test report follows the unified format. The parameter, the condition, the conclusion and the criterion are listed, and the same format supports the comparison and the archive.
The interface definition of the modular design is fixed first. The mechanical interface, the electrical interface and the communication interface are defined, and the module exchange loses the meaning without the unified interface.
The guide rail and the lock of the plug-in module are the wear parts. The repeated insertion deforms the rail and loosens the lock, the module positioning shifts, the contact face wears, and the periodic inspection replaces the worn parts.
The thermal design of the modular system is calculated at the worst configuration. The full configuration gives the largest thermal load, the margin is sized from the full load, and the fan speed is reduced for the light configuration.
The current sharing of the parallel modules is verified by the measurement. The sharing coefficient is measured at the rated load and the half load, and the light-load imbalance with the heavy-load sharing is not rare.