Flexibility of Polarity-Switchable High-Voltage Supply in Multi-Process Electrostatic Pilot Lines
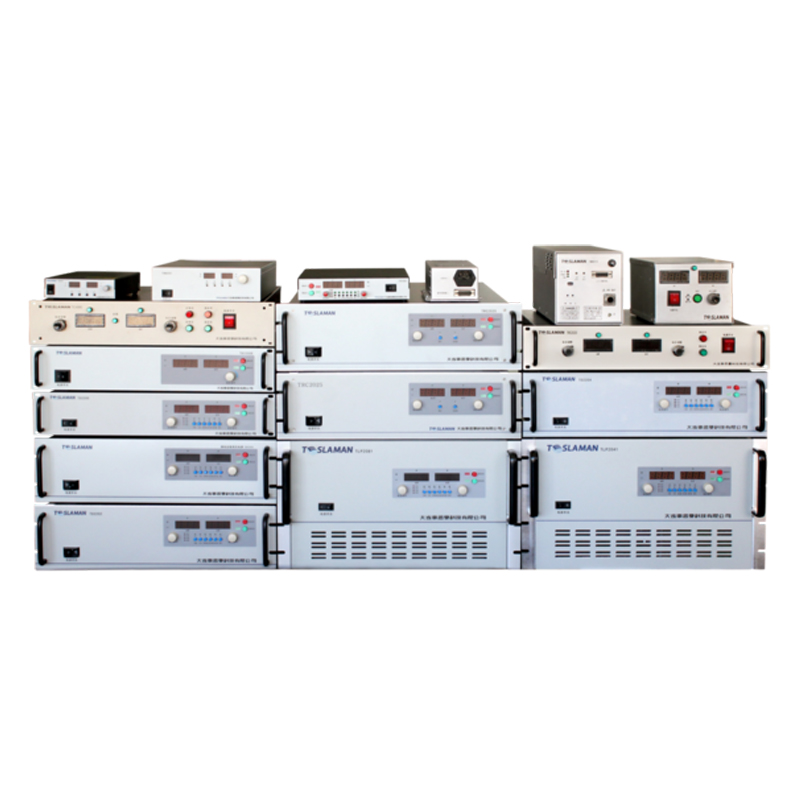
The flexibility of a polarity-switchable high-voltage supply determines how widely a multi-process electrostatic pilot line can be utilized. A pilot line typically combines electrostatic deposition, powder separation, surface spraying and charge neutralization inside one facility, and each step places different demands on output polarity, voltage amplitude and dynamic behavior. A supply that reverses polarity within a short interval enables a single power stage to serve multiple process configurations without exchanging equipment between trials. Such flexibility shortens changeover time, reduces floor space and simplifies the interface between process control and power electronics. The value of this capability grows as the number of process variants on the line increases, because parameter-based changes cost far less than hardware changes.
The first design requirement concerns the switching capability of the output stage. Polarity reversal involves discharging the parasitic capacitance of the high-voltage section and re-establishing the opposite field with controlled slew. The reversal interval must be consistent with process timing, and the peak transient must remain below the insulation rating of cables, connectors and process chambers. Switching losses at high repetition rates affect thermal design, so the commutation circuit must balance speed, efficiency and component stress. A carefully chosen commutation topology reduces the voltage stress on switching devices and preserves the reliability of the power stage over millions of reversal cycles.
The second requirement concerns output accuracy after reversal. Voltage set-point tolerance, load regulation and temperature drift all contribute to the final field strength applied to the process material. A multi-process line expects the supply to maintain the same accuracy in either polarity, which demands symmetrical feedback scaling and careful calibration of the sense network. Mismatched divider ratios between polarities produce systematic errors that become visible in coating thickness or separation efficiency. Regular verification of both polarities against a common reference keeps these errors within specification.
Insulation coordination forms the third requirement. The switching element, the isolating transformer and the feedback path must withstand the full reversal stress repeatedly over the equipment lifetime. Creepage distances, clearance and the selection of insulating materials follow the peak voltage rather than the nominal value, so derating margins must be verified under worst-case conditions. Partial discharge behavior at the switching node deserves particular attention because repeated transients accelerate aging of the insulation system.
The control architecture integrates polarity sequencing with process interlocks. A state machine coordinates the charge, reversal, stabilization and discharge phases, and each transition follows a defined ramp profile to avoid abrupt field changes. Interlocks prevent application of high voltage before the chamber conditions are ready. Digital control allows the ramp parameters to be stored per process recipe, so the same hardware serves trials with different timing requirements. Fault handling logic returns the output to a safe state and records the event for analysis.
Measurement and feedback design must preserve accuracy across the reversal event. The sense circuit should be insensitive to common-mode transients, and the sampling window should be synchronized with the stable portion of the output. Averaging over the ripple period improves the reported value, while fast detection of reversal faults provides immediate protection. Calibration procedures should verify both polarities against the same reference to guarantee symmetry, and the calibration data should be stored in the supply for traceability.
Verification covers functional, endurance and environmental aspects. Functional tests confirm reversal timing, transient magnitude and output accuracy under nominal load. Endurance tests apply repeated polarity cycling at the rated repetition rate and monitor the drift of timing and accuracy over a defined number of cycles. Environmental tests, including temperature and humidity exposure, confirm that insulation margins remain valid under field conditions. Acceptance criteria are defined before testing so that results can be judged objectively.
Integration with the pilot line includes communication, grounding and interference control. The supply exchanges status and commands with the line controller through a standard interface, and the grounding scheme prevents circulating currents between the power stage and the process chamber. Electromagnetic compatibility measures limit conducted and radiated interference so that sensitive instrumentation on the line remains unaffected during switching. Cable routing and shielding follow the integration guide to preserve the transient behavior measured in the laboratory.
The application value of polarity flexibility appears in faster process development. When a new formulation requires a different field configuration, the change is executed through parameters instead of hardware modifications. This shortens the iteration loop, allows parallel evaluation of process variants and makes the pilot line a flexible test bed for scale-up decisions. Operational costs also decrease because a single supply replaces several polarity-dedicated units, and spare-parts management becomes simpler with fewer distinct models.
Field experience confirms that maintenance and training requirements stay modest when the design is consistent. Operating manuals, fault tables and calibration guides are organized around the same control concept in both polarities, which reduces the learning effort for operators and technicians. Preventive maintenance focuses on the switching stage and the insulation system, and the diagnostics built into the supply indicate when attention is needed before a failure interrupts the process.
Operational data management adds further value to the pilot line. Each process run records the polarity sequence, voltage profile, transient behavior and environmental conditions, and these records are correlated with the quality data of the produced samples. The accumulated database supports analysis of how switching parameters influence process outcomes, allowing the line to converge on robust settings faster. When a quality deviation appears, the stored records shorten the search for the root cause, and the corrected settings are fed back into the recipe library. This closed loop turns the pilot line into a learning environment where every trial contributes to the knowledge base of the production scale-up.
Development directions continue toward shorter reversal times, wider voltage ranges and higher repetition rates. Advances in wide-bandgap switching devices reduce commutation losses, and improved insulation systems raise the sustainable transient level. Digital control and diagnostics bring self-verification features that report remaining insulation margin, supporting predictive maintenance on the pilot line. The flexibility of the supply will keep expanding as these technologies mature, allowing electrostatic processes to adapt to an ever wider set of products.