Adsorption Reliability of Electrostatic Chuck High-Voltage Supply in Vacuum Robot Hand and Wafer Fixing
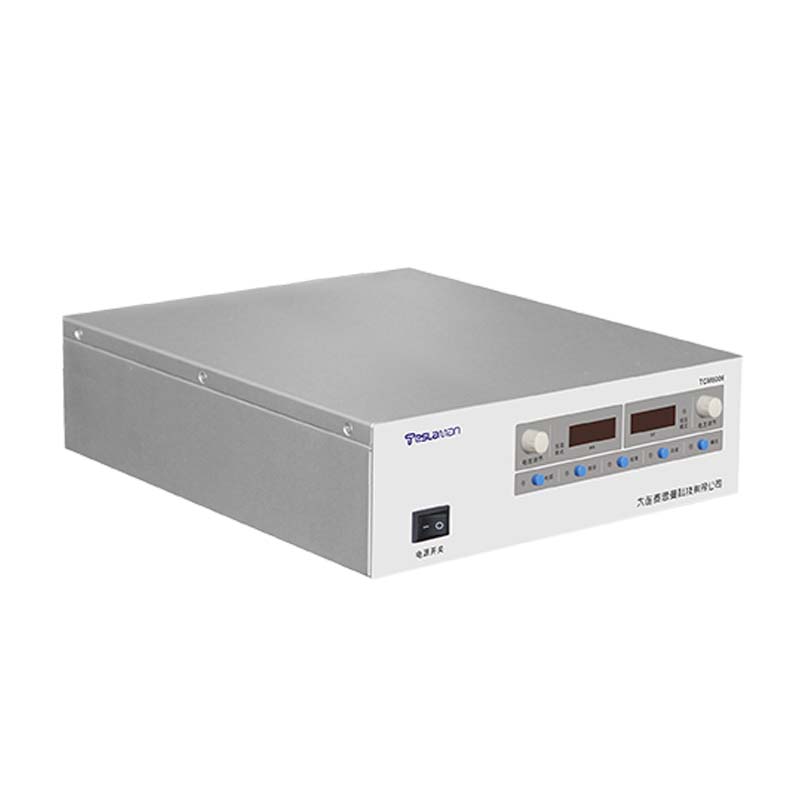
Electrostatic chucks in vacuum robot hands hold the wafer during transfer, and the adsorption reliability of the chuck determines the transfer success rate. The supply that powers the chuck must deliver a stable voltage, a controlled ramp, and a fast discharge, all within the mechanical timing of the robot.
The chuck capacitance is significant, and the voltage ramp controls the adsorption force transient. A fast ramp creates a large impact force that can shift the wafer on the chuck, while a slow ramp extends the transfer cycle. The ramp is programmed from the wafer weight and the transfer acceleration.
The adsorption force depends on the voltage and the gap between the wafer and the dielectric. The gap varies with the wafer flatness, so the same voltage produces different forces for different wafers. The supply cannot correct the gap, but the voltage set point is adjusted per wafer lot from the measured flatness data.
Voltage stability during the hold phase keeps the force constant. A voltage drift changes the force and allows a slow lateral displacement of the wafer during the transfer. The stability specification is set from the maximum acceptable displacement, and the measured drift is verified at the acceptance test.
The discharge phase must release the wafer without residual charge. A residual charge holds the wafer partially and delays the release, so the discharge sequence includes a polarity reversal to neutralize the surface charge. The discharge time is measured and matched to the robot timing.
Reliability in the vacuum environment adds constraints on the materials and the cooling. The supply electronics operate at the ambient temperature of the transfer chamber, and the thermal design is verified over the expected temperature range. The derating behavior protects the electronics during a thermal excursion.
Arc protection responds to a discharge between the chuck electrodes or between the chuck and the wafer. The detection circuit identifies the current transient and shuts the output down, and the recovery sequence restores the voltage after a defined delay. The arc count is logged as a diagnostic indicator.
Preventive maintenance covers the high-voltage cable, the connector, and the grounding path. The insulation resistance is measured at each maintenance interval, and a declining trend points to moisture or contamination inside the chuck assembly. The trend data schedule the chuck refurbishment.
Documentation control ensures that the drawings, the manuals, and the configuration records reflect the installed equipment. Any modification is documented with the change reason and the verification result. The document set is reviewed at planned intervals, and the obsolete versions are archived rather than discarded.
Spare parts management matches the stock level to the failure statistics of the equipment family. The fast-moving parts are kept on site, and the slow-moving parts are sourced on demand. The stock review is performed quarterly, and the review data include the part cost and the delivery lead time.
Safety procedures around the high-voltage equipment are written, reviewed, and rehearsed. The procedures cover the access control, the discharge sequence, and the use of personal protective equipment. The rehearsal results are recorded, and the procedure is revised when the rehearsal reveals a gap.
Environmental control in the equipment room stabilizes the operating conditions of the supply. The temperature and the humidity are monitored continuously, and the alarm thresholds are set to protect the insulation and the electronics. The environmental records are kept alongside the equipment log for the correlation analysis.
Data analysis turns the logged operating data into maintenance decisions. The voltage, current, temperature, and alarm trends are reviewed at planned intervals, and the deviations from the baseline trigger an investigation. The analysis report is shared with the engineering team and the maintenance crew.
Reliability assessment uses the field data collected from the equipment population. The failure rate, the repair time, and the availability are computed over a rolling period, and the results are compared with the design targets. The assessment output feeds the capital replacement plan and the spares strategy.
Energy efficiency of the supply affects the operating cost and the cooling load. The efficiency is measured at the representative operating points, and the improvement opportunities are evaluated against the implementation cost. The efficiency records are maintained for the lifetime comparison.
Training programs for the operating and maintenance staff are scheduled at defined intervals. The training covers the safe operation, the routine checks, and the fault diagnosis flow. The training effectiveness is verified with a written test and a practical exercise, and the results are filed with the personnel records.
Process qualification is performed whenever the equipment or the process recipe changes. The qualification plan defines the test articles, the acceptance criteria, and the data to be recorded. The qualification report is approved before the new condition enters production.
Failure analysis follows a defined path from the symptom to the root cause. The analysis uses the logged data, the physical evidence, and the repair records. The analysis conclusion is documented with the corrective action, and the corrective action is verified after implementation.
Quality records link the equipment performance to the product quality. The operating parameters and the product measurements are filed together, so that a product deviation can be traced to the equipment condition. The record retention period follows the regulatory and contractual requirements.
Vendor coordination covers the technical support, the spare supply, and the repair service. The service level agreement defines the response time and the repair turnaround. The vendor performance is reviewed periodically, and the review outcome influences the future procurement decisions.
Continuous improvement is driven by the analysis of the failure data and the operating experience. Each improvement proposal is assessed for the benefit, the cost, and the risk before implementation. The implemented improvements are tracked for the realized benefit.
Operator handover between shifts includes the equipment status, the pending issues, and the instructions for the current operation. The handover log is signed by both parties, and the entries are concise and factual. The handover discipline maintains the continuity of the operation.
Performance monitoring covers the key parameters that indicate the health of the supply. The monitoring points and the thresholds are defined during commissioning, and the measured values are recorded on a regular basis. The monitoring data support the early detection of the degradation trends.