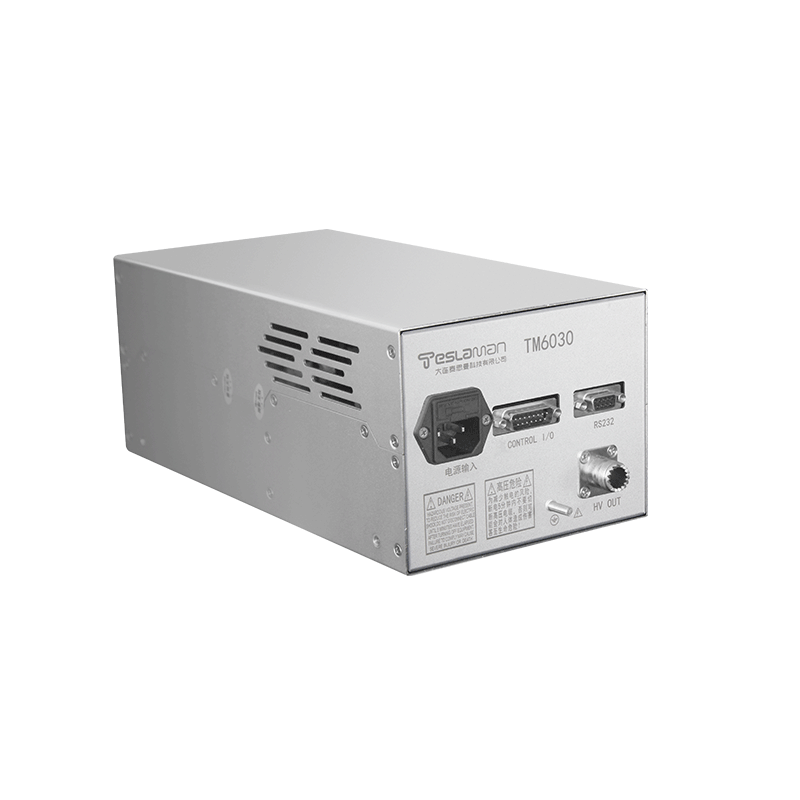
Insulation Performance Testing and Comparison of Electrostatic Chuck High-Voltage Power Supply in Vacuum Environments
Insulation performance testing of an electrostatic chuck supply in vacuum environments addresses the peculiar conditions of the vacuum chamber. The feedthrough and the cable run in vacuum, the heat removal is limited, and the insulation must hold under the combined electrical and thermal stress.
Vacuum insulation differs from atmospheric insulation. The breakdown path is set by the surface condition and the spacing rather than by the air gap, the test is performed in the actual vacuum environment, and the pressure level is recorded with the results.
The feedthrough is the most critical insulation element. The ceramic or polymer body carries the full voltage, the surface is kept clean, and the withstand test includes the feedthrough together with the cable so that the interface is verified as a system.
Outgassing of the insulation materials affects the vacuum quality. The materials are selected for low outgassing, the outgassing rate is measured during the test, and the result is compared with the chamber specification before the unit enters service.
Heat removal in vacuum relies on conduction and radiation. The cable and the feedthrough carry the dissipation, the conductor cross-section is sized for the current, and the temperature rise is verified under the rated load in vacuum.
Partial discharge in vacuum appears at lower levels than in air for the same voltage. The discharge is measured with a sensitive detector, the inception voltage is recorded, and the margin between the inception and the rated voltage is documented.
Voltage cycling in vacuum stresses the surface insulation. The voltage is ramped and held repeatedly, the leakage current is measured at each hold, and a rising leakage trend indicates surface contamination that requires cleaning.
The comparison between vacuum and atmospheric results guides the design margin. The derating factor between the two environments is measured, the operating voltage is set with the margin, and the test data justifies the derating value.
Moisture is released into the chamber after venting. The chamber pump-down removes the moisture, the supply is energized only after the pressure reaches the specified level, and the interlock enforces the pressure condition before high voltage is applied.
Repeated vent and pump cycles age the feedthrough seal. The seal condition is inspected at the scheduled maintenance, the insulation resistance is measured after each cycle, and the inspection record tracks the aging trend.
Field failures at the feedthrough often trace to mechanical stress. The cable must not pull on the feedthrough, the support and the strain relief are checked, and the mechanical design is verified by the endurance test.
The complete insulation test record includes pressure, temperature and voltage data. The archive supports the comparison between units, the trend analysis of the installed fleet, and the replacement decision for the feedthrough assemblies.
Product consistency is guarded by factory testing. Voltage accuracy, ripple, protection action and temperature rise are verified unit by unit, test data is archived, and batch variation is analyzed statistically.
Spare parts management follows the failure statistics. High-failure parts carry higher stock, long-lead parts are reserved in advance, and downtime shortens.
The remote maintenance channel needs security design. Permission levels, operation audit and data encryption are enforced, remote operations confirm the site condition first, and misuse risk stays bounded.
Residual charge discharge time at the output enters the safety procedure. Maintenance starts after the discharge completes, and the discharge indicator works with the mechanical interlock.
Online and offline insulation measurements complement each other. Online monitoring reflects the dynamic state, offline measurement gives absolute values, and the combination evaluates insulation health.
High-frequency noise is suppressed through the dual channels of shielding and filtering. Shielding blocks the radiation path, filtering attenuates the conducted path, and the two together meet the whole-unit specification.
Process parameters and supply parameters are archived together. Recipe numbers, voltage and current settings and batch results are linked, parameter changes leave traces, and quality traceability stays complete.
Insulation coordination starts with field distribution control. Electrode radii and shield placement determine the local field stress, and weak points show discharge precursors first. Field simulation verifies the stress margin at the design stage, and withstand testing confirms the result on the finished unit.
Filter network parameters balance ripple rejection against dynamic response. Larger output capacitance improves ripple but lengthens the voltage settling time, so the operating point is set from the actual load requirements rather than from a generic rule.
Thermal management decides power device lifetime. Losses concentrate in the switching devices and the magnetic components, and the heatsink thermal resistance plus the airflow path are sized for the worst-case duty. Temperature sensors are placed from the thermal analysis, and the data feeds the derating logic.
The reference and the divider network form the basis of voltage accuracy. The reference is selected for low drift, the divider resistors are matched, and the assembly is sealed against humidity. Calibration data is archived and periodic re-verification holds long-term precision.
Grounding practice controls the noise floor of control and measurement. Signal ground, power ground and chassis ground meet at a single point, ground loops are eliminated, and shield terminations follow a defined rule. Field commissioning verifies the grounding integrity before noise targets are assessed.
Protection timing matters as much as the protection itself. Hardware comparators cover microsecond fast response, software logic handles sustained faults, and the two layers cover different time scales. Action records support post-event analysis.
Electromagnetic compatibility is handled from the layout stage. Power lines, sampling lines and control lines run in separate routes, shields are terminated correctly, filter components sit close to the disturbance source, and conducted and radiated tests confirm the result.
Long-term drift monitoring adds more value than a single calibration. Output readback values are recorded as a time series, trend analysis reveals acceleration of drift, and predictive maintenance intervenes before failure, which reduces unplanned downtime.
Field commissioning starts with the supply conditions. Input voltage range, grounding resistance and grid harmonics determine the observed behavior of the supply, and control tuning cannot converge while supply-side problems remain unresolved.
Insulation material aging defines the maintenance interval. Dielectric strength, temperature rating and moisture resistance are selected for the working conditions of each part, aging test data supports the replacement plan, and insulation monitoring tracks the running state.
Soft-start control protects the power stage and the load. The voltage rises along a defined slope, the inrush current stays bounded, the establishment time matches the process cycle, and an abnormal start is aborted to a safe state.