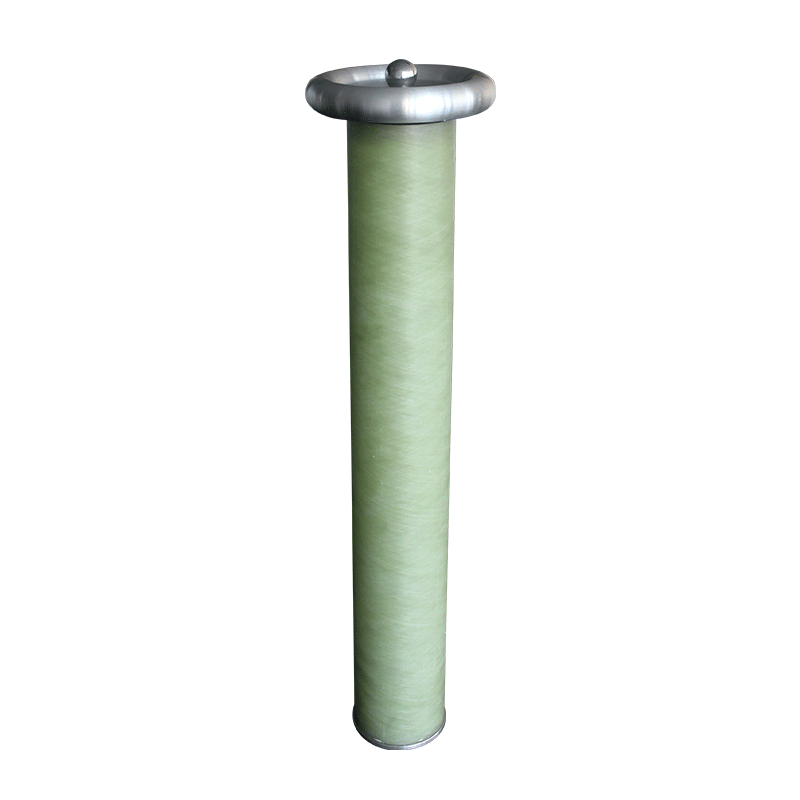
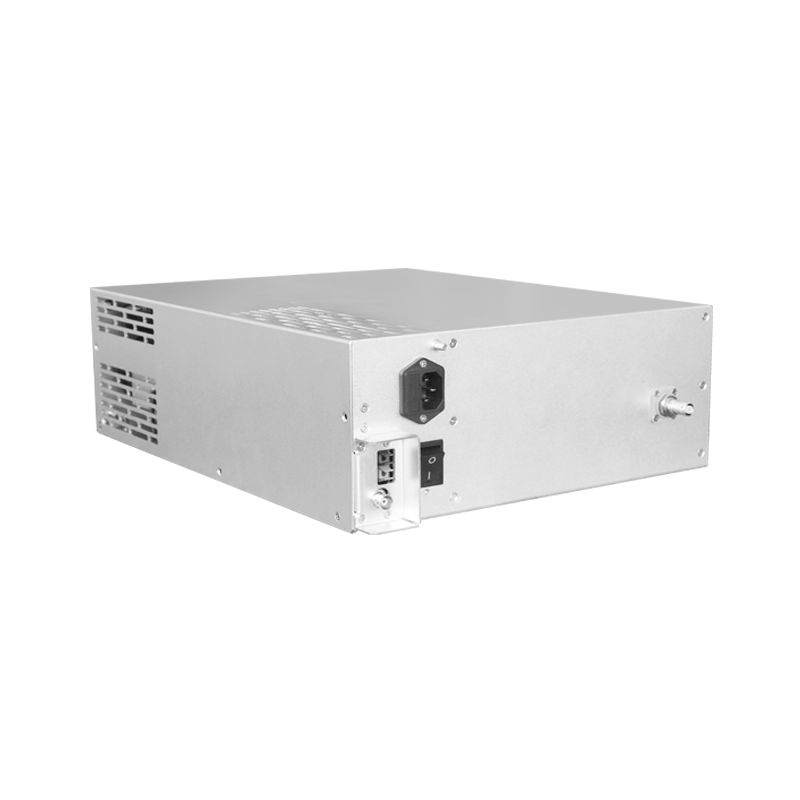
Excimer Laser High-Voltage Power Supply Energy in Mask Repair and Laser Marking Systems
Mask repair and laser marking place different demands on the excimer laser high-voltage supply, but both applications require pulse-to-pulse energy stability. In mask repair the energy error must stay small enough that the removed material volume does not vary between pulses, while marking applications tolerate wider variation but need long-term consistency across a production run. The common engineering problem is the regulation of the charging voltage that stores the pulse energy.
The storage capacitor voltage sets the energy available for the discharge, and the regulation loop must bring that voltage to the target within the inter-pulse interval. Charging accuracy better than one percent of the target voltage keeps the pulse energy within the required band. Field measurements on a repair system show that a charging accuracy of half a percent reduces the rejected work by a measurable margin over a month of operation.
Gas mixture aging shifts the breakdown voltage of the discharge chamber, and the charging voltage must compensate for the shift to keep the deposited energy constant. The compensation curve is established during commissioning and refined with the operating hours. Without compensation the pulse energy drifts upward or downward as the gas ages, and the process window narrows accordingly.
The repetition rate of the supply interacts with the charging time in the same way as in any pulse system. A higher repetition rate leaves less time for charging, and the charging stage must deliver the energy faster without losing accuracy. The trade-off between repetition rate and energy stability is settled by the application requirements, and the supply is configured accordingly at installation.
Trigger synchronization between the charging cycle and the discharge command determines the consistency of the pre-ionization interval. A jitter in the trigger path translates into a variation of the discharge timing and a corresponding variation of the pulse energy. The trigger circuitry should be designed with controlled impedance and verified with an oscilloscope during commissioning.
High-voltage components in the discharge loop experience repeated current stress, and the condition of these components governs the long-term energy stability. The discharge switch, the snubber network, and the capacitor connections should be inspected at planned intervals. The inspection records form a trend that supports the predictive replacement of the stressed components.
Electromagnetic interference from the discharge loop affects the nearby control electronics, and the layout of the high-voltage section should keep the discharge loop compact. A compact loop radiates less and couples less into the measurement circuitry. Shielding around the discharge section and filtering on the control inputs complete the interference management.
Cooling of the high-voltage section is a practical concern at elevated repetition rates. The charging stage and the discharge switch dissipate heat, and the cooling path must remove that heat to keep the component temperatures within limits. A blocked cooling path shows up as a slow drift of the pulse energy before the drift becomes a hard failure.
Maintenance records for the excimer supply include the gas history, the voltage settings, and the energy measurements, because these quantities interact. A sudden change in the required charging voltage often indicates a gas or electrode problem rather than a supply fault. The correlation between the logged voltage and the process results helps the maintenance crew distinguish supply issues from chamber issues.
Safety interlocks around the high-voltage supply protect the personnel who work near the laser system. The interlocks should cover the enclosure access, the discharge state, and the stored energy level. The interlock logic is tested periodically, and the test results are recorded.
Operator training for the excimer system covers the interpretation of the energy monitor readings. The operators should know the normal range of the charging voltage for the current gas condition and recognize the signs of gas aging. Training includes the safe discharge procedure used before opening the high-voltage enclosure.
The long-term operating cost of the excimer supply includes the energy consumption, the gas replacement, and the component replacement. The energy stability of the supply influences the gas lifetime because an unstable discharge ages the gas faster. A stable supply therefore reduces both the energy cost and the gas cost over the equipment life.
Field experience feedback collects the observations from the operating sites and feeds the observations into the design and the maintenance practice. The feedback items are categorized and reviewed at the defined intervals. The implemented feedback is documented in the equipment history.
Periodic review of the equipment covers the performance, the maintenance, and the cost since the last review. The review findings are summarized into the recommendations for the next period. The review is scheduled annually or when a significant event occurs.
Commissioning of the supply begins with a visual inspection of the high-voltage section and the cooling path, followed by a no-load voltage check and a load test at the rated output. The acceptance data are recorded against the specification table, and any deviation is resolved before the equipment enters service. The commissioning report becomes the baseline for all later comparisons.
Acceptance testing covers the electrical performance, the protective functions, and the mechanical integrity. The test sequence is defined in the procurement document, and each test has a pass criterion. The signed acceptance record accompanies the equipment through the service life and supports the warranty claims when a defect appears.
Long-term stability of the supply is verified by the periodic re-measurement of the output characteristics. The measurements are compared with the baseline recorded at acceptance, and the drift trend is analyzed. A drift beyond the tolerance triggers a detailed investigation and a corrective action.
Troubleshooting flow guides the maintenance crew from the symptom to the probable cause. The flow is built from the documented fault cases and the component knowledge. The use of the flow shortens the diagnosis time and reduces the trial-and-error work.
System integration between the supply and the process controller is validated with the interface tests. The signal definitions, the timing, and the fault propagation are verified under the representative conditions. The integration records are kept with the system documentation.
Field experience feedback collects the observations from the operating sites and feeds the observations into the design and the maintenance practice. The feedback items are categorized and reviewed at the defined intervals. The implemented feedback is documented in the equipment history.